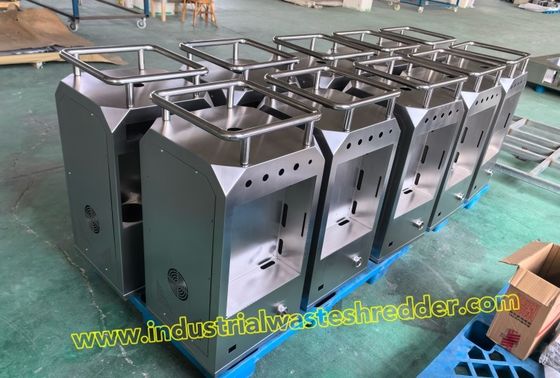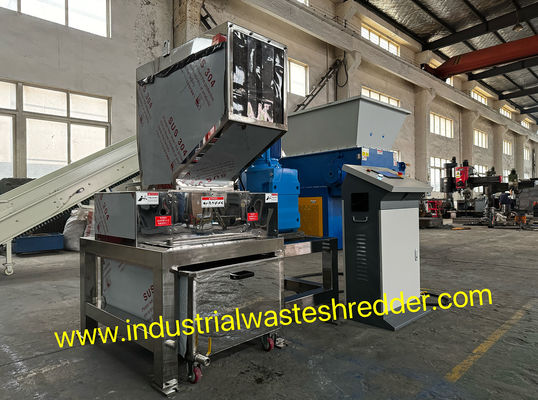
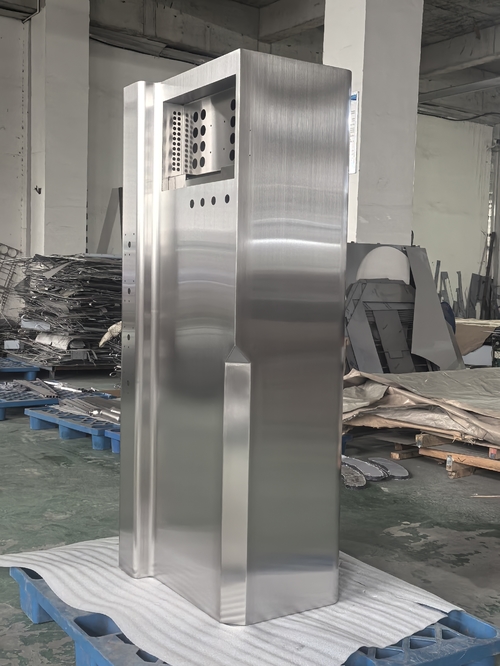
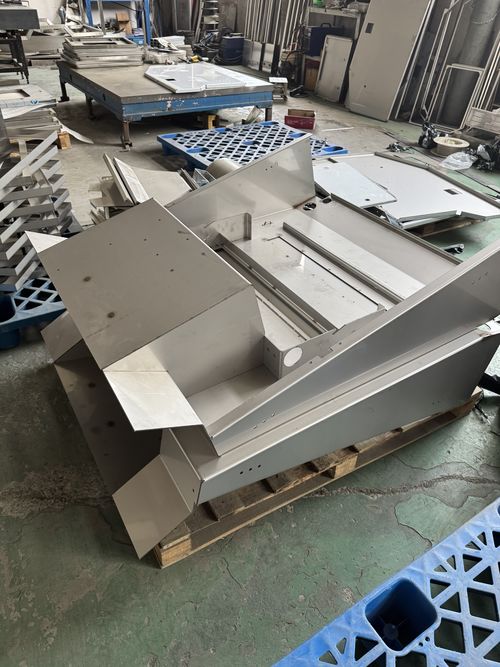
Project snapshot: a UK manufacturer of recycling and material sorting equipment needed a stainless steel fabrication partner for 316L hoppers, guards and control enclosures. Over 14 months the project moved from a single trial order to a quarterly release schedule, with lead time reduced by 35% and first-pass yield raised from 88% to 98.5%.
Client Background
ItemDetail
IndustryRecycling and material sorting equipment
LocationUnited Kingdom
Company sizeMid-sized OEM, 120 to 150 staff
Parts in scope316L hoppers, side guards, control cabinets, mounting frames
Annual volumeAround 2400 fabricated assemblies
Service usedOEM sheet metal fabrication, welding, powder coating, kitting
The Problem
The client had been buying fabricated 316L parts from a local UK subcontractor. Three issues kept repeating. First, delivery slipped: quoted at 8 weeks, actual delivery ran to 12 weeks in peak season, which pushed machine assembly dates and forced expensive overtime. Second, weld quality was inconsistent. Hoppers that must hold liquid were failing leak tests on roughly one unit in eight, and rework had to be done after powder coating, which meant stripping, re-welding and recoating. Third, dimensional drift appeared on multi-part assemblies: brackets that passed inspection individually would not line up on the assembly line, because each part had been made from a different drawing revision.
Cost per part looked acceptable on paper, but the true cost including rework, line stoppage and air freight for urgent replacement parts was far higher than the purchase price suggested.
What We Changed
Drawing and revision control: one master drawing set was locked at project start, and every batch was produced against the same revision with a revision stamp on each part
Welding fixtures: jigs were built for the three highest-volume weldments so hoop distortion stayed within 1.5mm and leak tests became repeatable
First article approval: a full first article with CMM dimensional report and weld photographs was approved before any batch production
Material traceability: 316L mill certificates were filed per heat number and referenced on the packing list
Kitting: parts for one machine were packed and labelled as a kit rather than as bulk quantities, cutting line-side sorting time
Surface treatment: powder coating applied after all welding and leak testing, with 480-hour salt spray verification on test coupons
Execution Timeline
Week 1: drawing review, DFM report issued with 11 cost and quality suggestions
Week 2: quotation approved, NDA signed, welding jigs designed
Week 3 to 4: first articles produced and shipped by air for approval
Week 5: client engineering sign-off, minor bend radius change incorporated
Week 6 onwards: batch production in 3-week cycles, sea freight with 2 weeks buffer stock at client site
Results After 14 Months
MetricBeforeAfter
Average lead time12 weeks7.5 weeks
First-pass yield88%98.5%
Leak test failures per batch12 unitsFewer than 1 unit
Rework and recoating costBaselineDown 42%
Emergency air freight events5 per year0 in 14 months
Assembly fit-up complaintsRecurringNone since batch 2
Client Feedback
"The difference is predictability. We stopped building buffer stock to protect our assembly line, because the parts arrive when promised and they fit the first time," said the client's purchasing manager. "The DFM notes in the first quote paid for themselves in the first three batches."
Why The Project Worked
Three things made the difference: fixtures instead of skill-dependent welding, one locked drawing revision across every batch, and inspection data shipped with the parts so the client could verify rather than guess, and a single English speaking engineer accountable for the account.
Similar Project?
We fabricate 304 and 316L parts for recycling equipment, food machinery, medical housings and water treatment systems. Send your drawing with material, thickness, finish and annual quantity, and our engineering team will reply with a costed quotation and DFM notes within 12 working hours.
솔루션 | 我们的解决方案
✨ 고객이 정밀성, 품질 및 납품과 관련된 문제를 해결할 수 있도록 엔드 투 엔드 스테인리스 스틸 판금 제작 서비스를 제공합니다.
✅ 주요 솔루션 | 核心解决方案
맞춤 제작 | 定制加工도면 또는 샘플을 기반으로 맞춤형 스테인리스 스틸 판금 부품 제작.根据图纸或样品定制不锈钢钣金零部件.
정밀성 및 품질 관리 | 精度与质量管控출하 전 엄격한 공차 관리 및 100% 검사.严格公差管理,出货前100%检验.
유연한 생산 | 灵活生产프로토타입부터 대규모 주문까지, 고객의 요구에 맞춰 조정합니다.从打样,小批量到大批量生产均可支持.
빠른 리드 타임 | 快速交付긴급 일정을 충족하기 위한 신속한 프로토타입 제작 및 효율적인 생산.快速打样,高效生产,满足紧急交期.
원스톱 서비스 | 一站式服务설계 지원, 레이저 절단, 벤딩, 용접, 표면 마감 및 조립.提供设计支持,激光切割,折弯,焊接,表面处理到总装配的全流程服务.
전문 스테인리스 스틸 판금 제조 업체로서, 맞춤형 장비 인클로저에 대한 엔드 투 엔드 가공 서비스를 제공합니다. 원자재 시트에서 완전히 조립되고 마감된 제품까지, 각 단계는 국제 품질 표준을 충족하기 위해 정밀하게 완료됩니다. 다음은 스테인리스 스틸 장비 하우징을 생산하는 일반적인 워크플로우입니다:
1. 재료 선택 및 절단
고품질 스테인리스 스틸 시트(예: SS304 또는 SS316)를 선택하는 것으로 시작합니다. 고객의 도면에 따라, 정확한 치수와 깨끗한 가장자리를 얻기 위해 레이저 절단, CNC 쉐어링, 또는 펀칭을 사용하여 재료를 가공합니다.
2. 벤딩 및 성형
절단된 부품은 CNC 프레스 브레이크를 사용하여 성형하여 정확한 벤딩 각도와 일관된 공차 관리를 보장합니다. 복잡한 형태는 다단계 벤딩 또는 롤링 공정을 통해 얻을 수 있습니다.
3. CNC 가공 및 2차 가공
더 높은 정밀도 또는 특수 기능이 필요한 구성 요소의 경우, 상세한 기능 요구 사항을 충족하기 위해 CNC 밀링, 탭핑, 카운터싱킹, 및 드릴링을 수행합니다.
4. 용접 및 조립
구조적 요구 사항에 따라 부품을 접합하기 위해 TIG 용접, MIG 용접, 스폿 용접, 또는 스터드 용접을 사용합니다. 용접 후, 구성 요소를 조립하여 적합성과 안정성을 확인합니다.
5. 표면 처리
외관과 내구성을 향상시키기 위해 다음과 같은 여러 가지 마감 옵션을 제공합니다:
연마 및 광택
브러싱
샌드블라스팅
패시베이션 또는 지문 방지 코팅
이러한 처리는 내식성을 향상시키고 필요한 시각적 효과를 얻습니다.
6. 품질 검사
각 부품은 엄격한 치수 검사, 용접 품질 검사 및 기능 테스트를 거칩니다. 당사의 품질 팀은 모든 구성 요소가 포장 전에 고객 사양 및 국제 표준을 충족하는지 확인합니다.
7. 최종 포장 및 출하
완성된 인클로저는 세척되고 필름/폼으로 보호되며, 글로벌 고객에게 안전하게 배송하기 위해 수출용으로 안전하게 포장됩니다.